Starting from ₹800 / hour

CNC Machining

3-axis and 4-axis CNC milling and turning — complex geometries in aluminium, steel, brass, PEEK, and more. Tolerance ±0.025 mm.

Precision CNC Milling & Turning

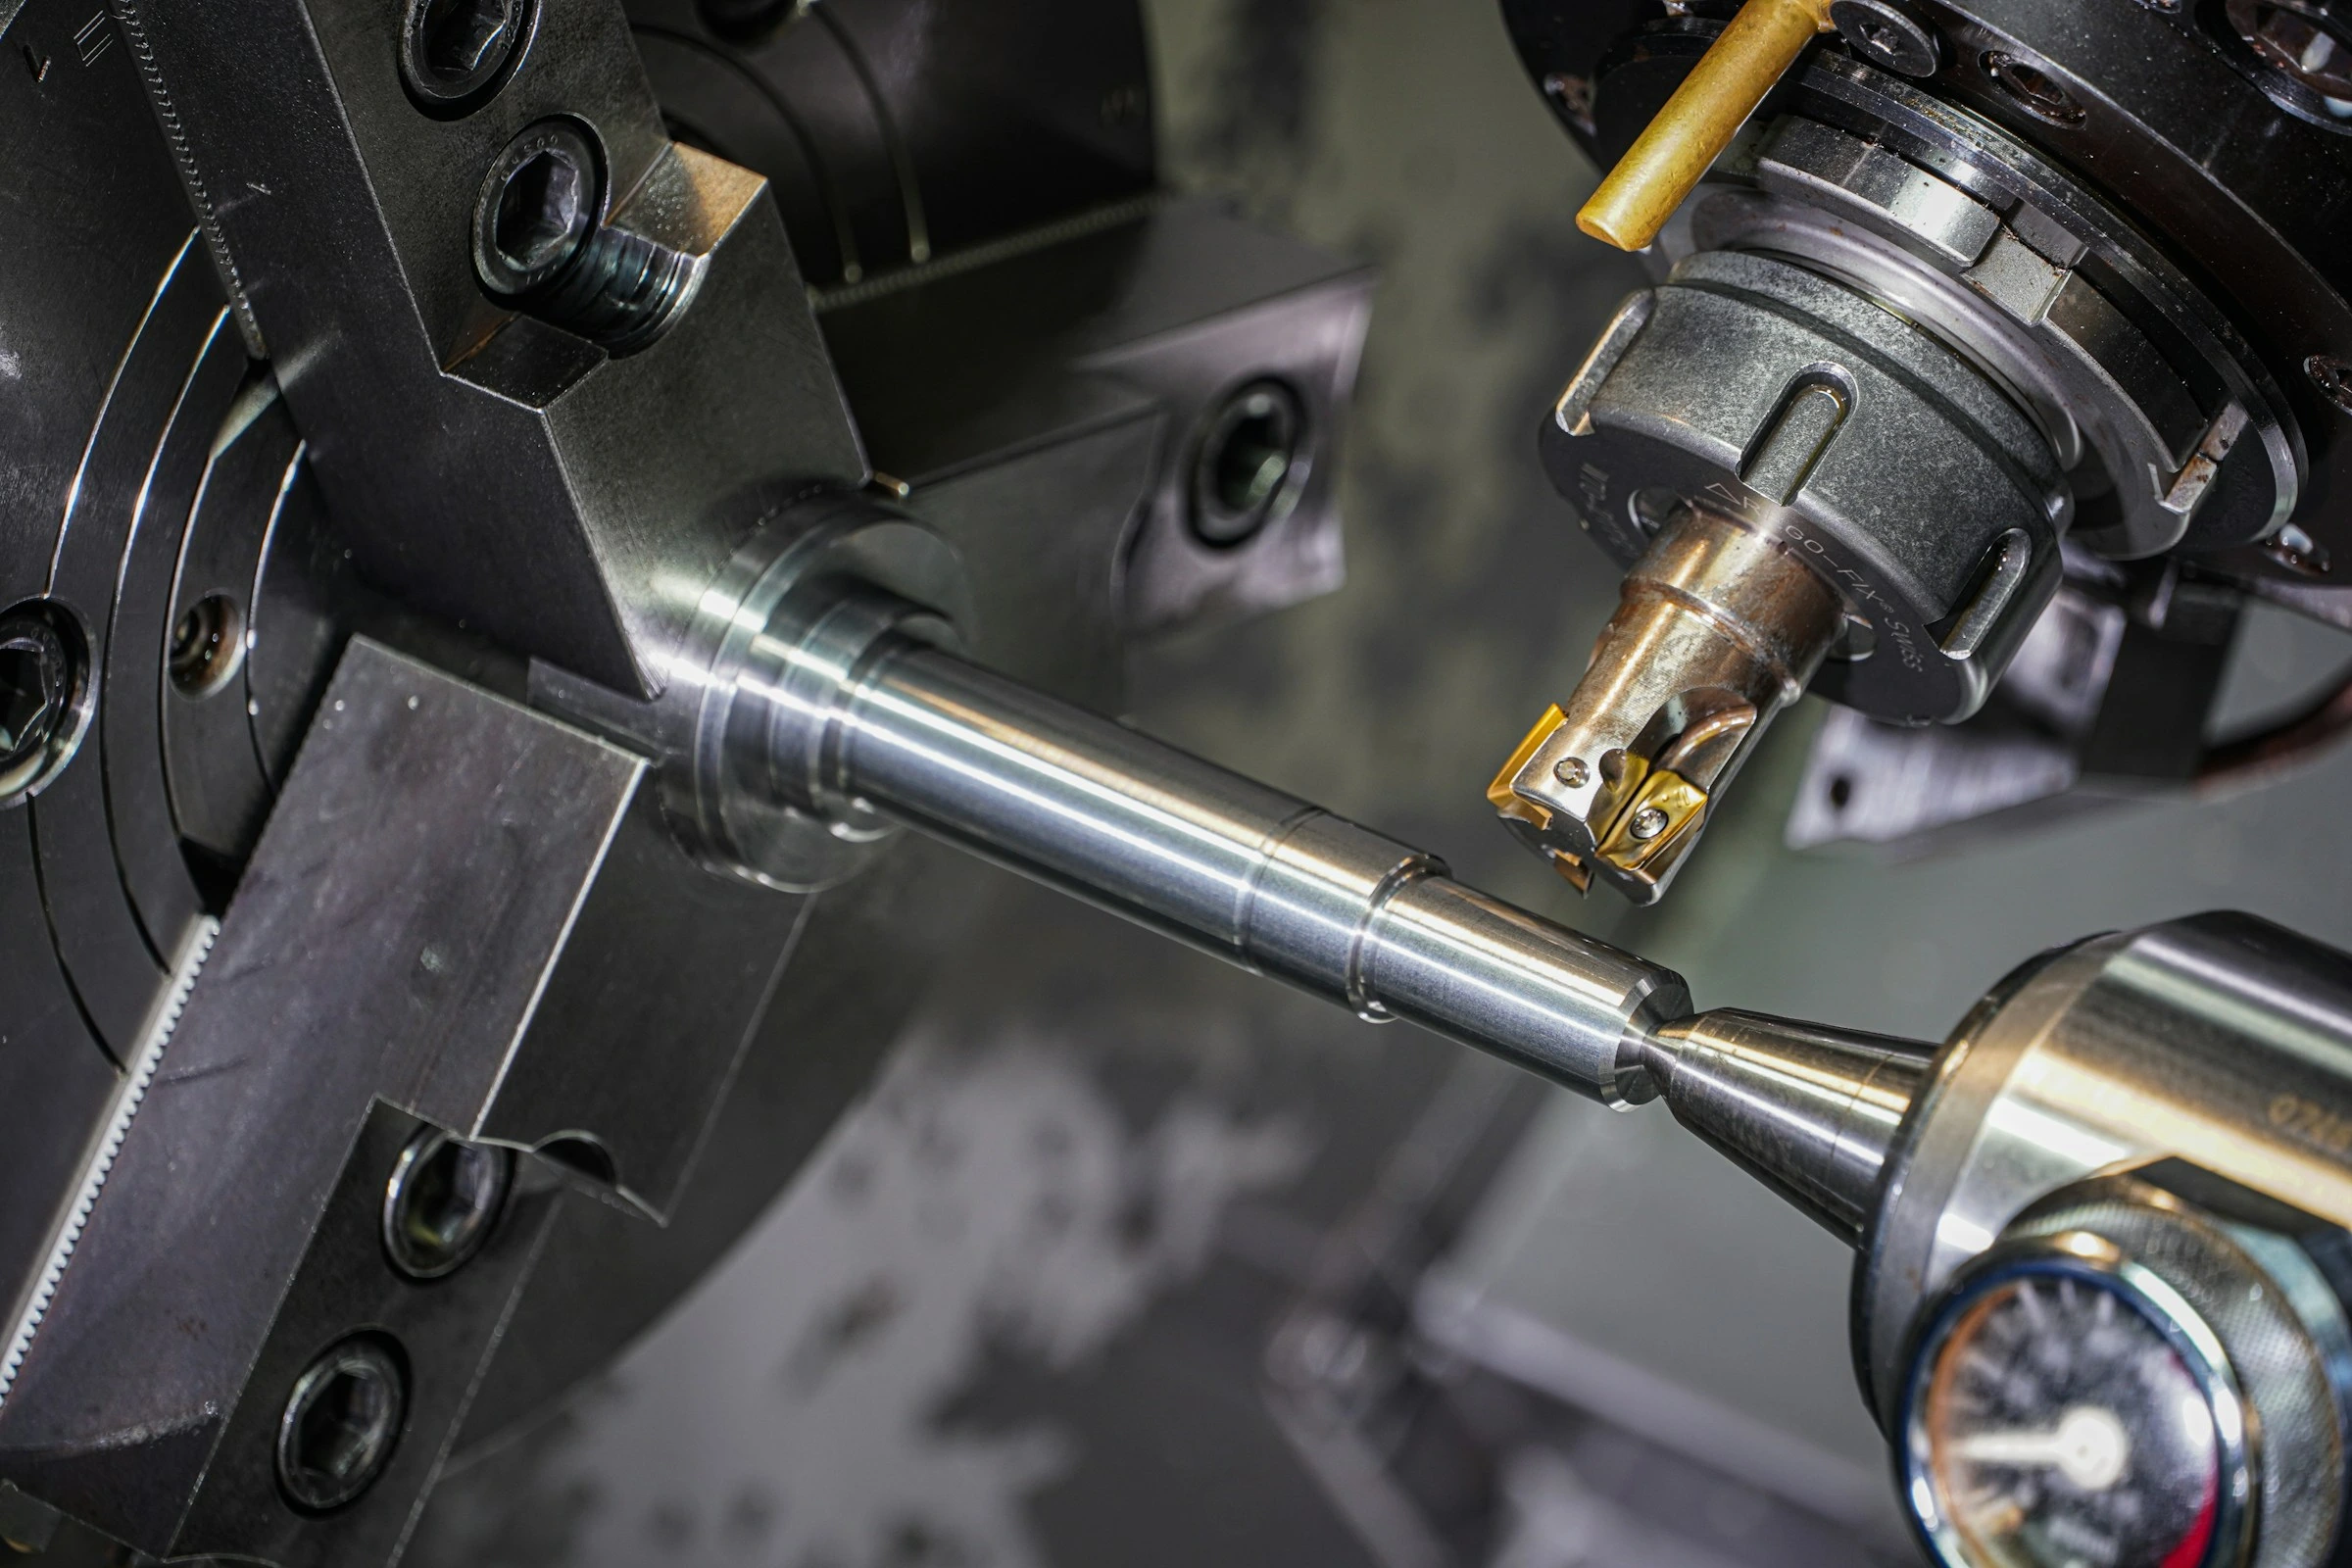
CNC machining removes material from a solid billet using computer-controlled cutting tools. FYORD runs 3-axis machining centres for prismatic parts and 4-axis for complex contours, plus CNC lathes for turned components.

Ideal for brackets, housings, shafts, flanges, heat sinks, jigs, and fixtures where sheet metal isn't enough. Tolerances tighter than ±0.025 mm achievable on request.

  • Milling max envelope: 500 × 300 × 150 mm
  • Turning max: Ø300 mm × 600 mm between centres
  • Surface finish Ra 0.8 – 3.2 µm standard
  • Thread milling, tapping, boring, and reaming in-house
  • ISO 2768 medium tolerance as standard
CNC machining close-up

Machine Specifications

Milling Envelope
500×300×150
mm (X×Y×Z)
Turning Max
Ø300 × 600
mm diameter × length
Tolerance
±0.025 mm
ISO 2768-m standard
Surface Finish
Ra 0.8 µm
Standard Ra 3.2 µm
Lead Time
3–7 days
Complex parts 7–10 days
File Formats
STEP · IGES
STL, DXF for 2D turning

Compatible Materials

MaterialGradeMachinabilityBest For
Aluminium6061-T6, 7075-T6 ExcellentEnclosures, heatsinks, brackets
Mild SteelEN8, EN19, A36 GoodStructural, jigs, fixtures
Stainless Steel304, 316L ModerateFood, pharma, marine
BrassCuZn39Pb3 (C360) ExcellentFittings, connectors, valves
Delrin / PEEKAcetal, PEEK GoodWear parts, insulators

DFM Rules for CNC Parts

Cavity Depth-to-Width

Keep pocket depth ≤ 4× cutter diameter. Deep narrow pockets require special tooling and add cost. Wide shallow pockets machine faster.

Corner Radii

Internal corners need a radius ≥ tool radius. Specify R3 mm or larger where possible. Sharp internal corners require EDM — quote separately.

Wall Thickness

Minimum wall thickness 0.8 mm for aluminium, 1.0 mm for steel. Thin walls vibrate during machining and reduce accuracy.

Hole Standards

Specify drilled holes by standard drill sizes (e.g. M3 clearance = Ø3.2). Blind holes should be ≥ 3× diameter deep. Specify thread class (6H/6g).

Datum & GD&T

Mark your primary datum face clearly. We machine to ASME Y14.5 GD&T if specified. Include a 2D drawing with critical tolerances called out.

File Preparation

Upload STEP or IGES 3D model. Include a 2D PDF with all tolerances, surface finish callouts, and material / heat treatment spec.

Pro tip: Adding a DXF 2D drawing alongside your STEP file cuts quoting time in half — our engineers can confirm tolerances without guessing.

Machining Rates

3-Axis Milling
₹800
per hour + material
  • Aluminium & mild steel
  • Standard Ra 3.2 finish
  • ISO 2768-m tolerance
High-Precision
Custom
tolerance ±0.01 mm
  • Gauge-grade surfaces
  • CMM inspection report
  • Net-30 payment terms

Frequently Asked Questions

What 3D file formats do you accept?
We accept STEP (.stp/.step) and IGES (.iges/.igs) for 3D models. For 2D turned parts, DXF or PDF with dimensions is fine. Always include a 2D drawing PDF for parts with GD&T or critical tolerances.
What is the tightest tolerance you can hold?
Standard is ISO 2768-m (±0.1 mm on linear, ±0.1° on angular). We routinely hold ±0.025 mm on milled features and ±0.01 mm on turned diameters. Tighter tolerances are possible with extra setup time — quote accordingly.
Do you provide inspection reports?
Yes — a basic dimensional check is included on all orders. A full CMM report (first article inspection) is available for ₹2,500 per part number. Our CMM is calibrated to NABL-traceable standards.
What is the minimum order quantity?
Minimum order value is ₹2,000. We machine single prototypes every day. Setup charges apply for quantities under 5 pieces — these are included in your quote automatically.

Ready to machine your parts?

Upload a STEP file and get a quote from our team within 2 hours.

Sign In Get Instant Quote →